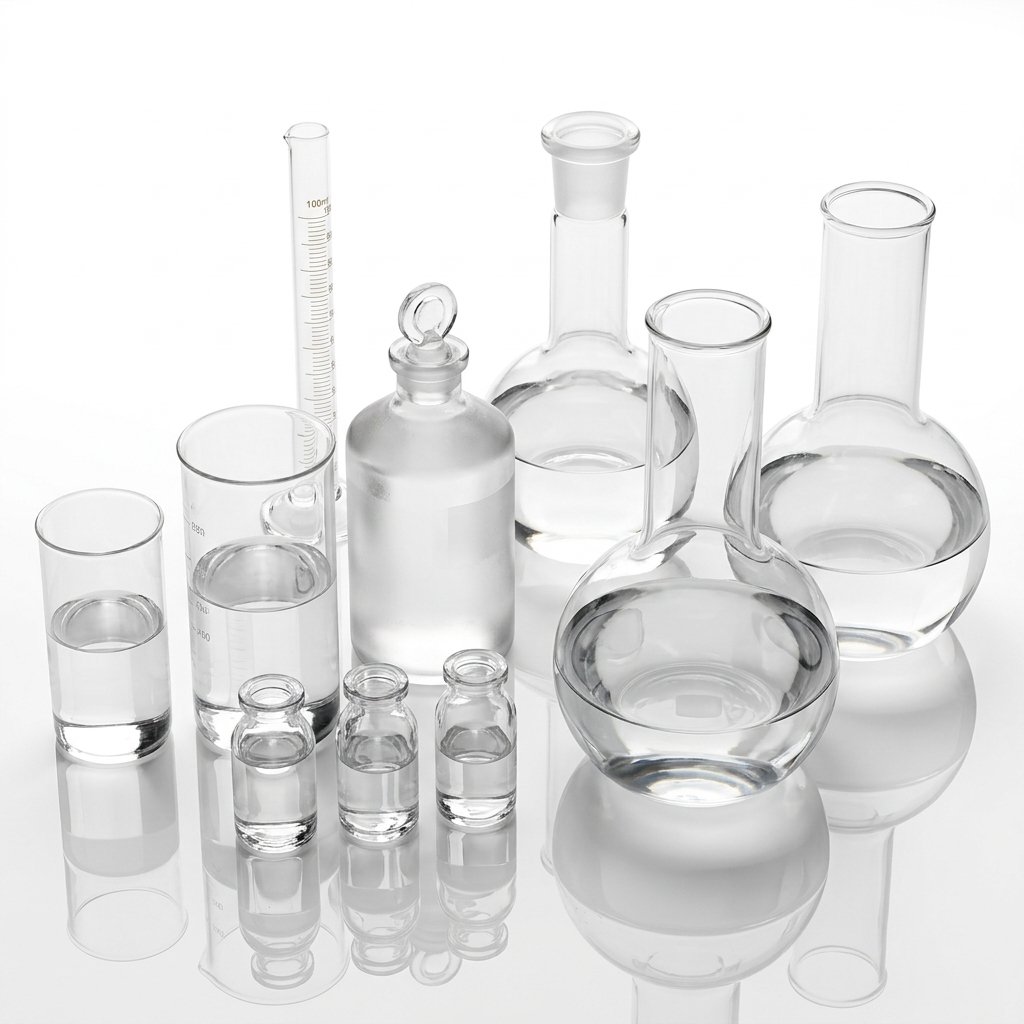
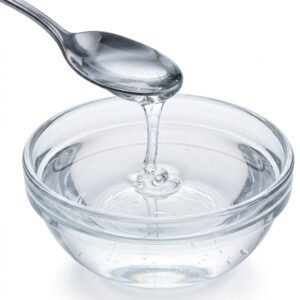
Ensure absolute purity and reliability in your manufacturing processes with Pharmaceutical & Industrial Grade Ethanol. Also widely known as ethyl alcohol, grain alcohol, or pure alcohol, ethanol is a clear, colorless liquid valued across the healthcare, pharmaceutical, cosmetic, and chemical industries.
Produced through natural plant fermentation or the hydration of ethylene, high-grade ethanol serves as an essential solvent, antiseptic agent, and chemical intermediate for manufacturing liquid medicines, tinctures, topical disinfectants, and personal care formulations.
Key Features & Benefits:
-
Exceptional Purity & Clarity: A premium clear, colorless liquid manufactured to meet stringent industrial and pharmaceutical specifications.
-
Versatile Application: Ideal as a high-performance solvent, sterilizing agent, extraction medium, and chemical intermediate for pharmaceutical preparations and cosmetics.
-
Reliable Shelf Stability: Formulated for consistent chemical integrity, guaranteeing a dependable shelf life of up to 2 years under recommended storage conditions.
-
Industrial Bulk Packaging: Securely packaged in robust 300 kg containers, designed to support large-scale commercial production and manufacturing workflows efficiently.
Product Attributes / Specifications
| Attribute Name | Details / Options to Add |
| Product Type | Ethanol / Ethyl Alcohol / Grain Alcohol (Pharmaceutical & Industrial Grade) |
| Appearance | Clear, Colorless Liquid |
| Primary Uses | Solvent, Antiseptic, Extraction Medium, Pharmaceutical Intermediates |
| Shelf Life | 2 Years |
| Pack Size | 300 kg Drum / Container |
| Minimum Order Quantity (MOQ) | 300 kg |
| Brand | Nexgencare Limited |
Reviews
There are no reviews yet.